How Research Peptides Are Manufactured for Labs
A peptide label can look simple: sequence, quantity, lot number, purity claim. The work behind that label is not simple. How research peptides are manufactured determines whether a material is traceable, analytically supported, and consistent enough to enter a serious research workflow. No shortcuts.
For laboratory buyers, manufacturing quality is more than a marketing point. A synthesis impurity, an incorrectly identified peak, poor moisture control, or incomplete lot documentation can introduce avoidable variables into a study. Reliable peptide manufacturing is a controlled chain of decisions, testing, and release criteria from sequence design through final packaging.
How Research Peptides Are Manufactured: The Core Process
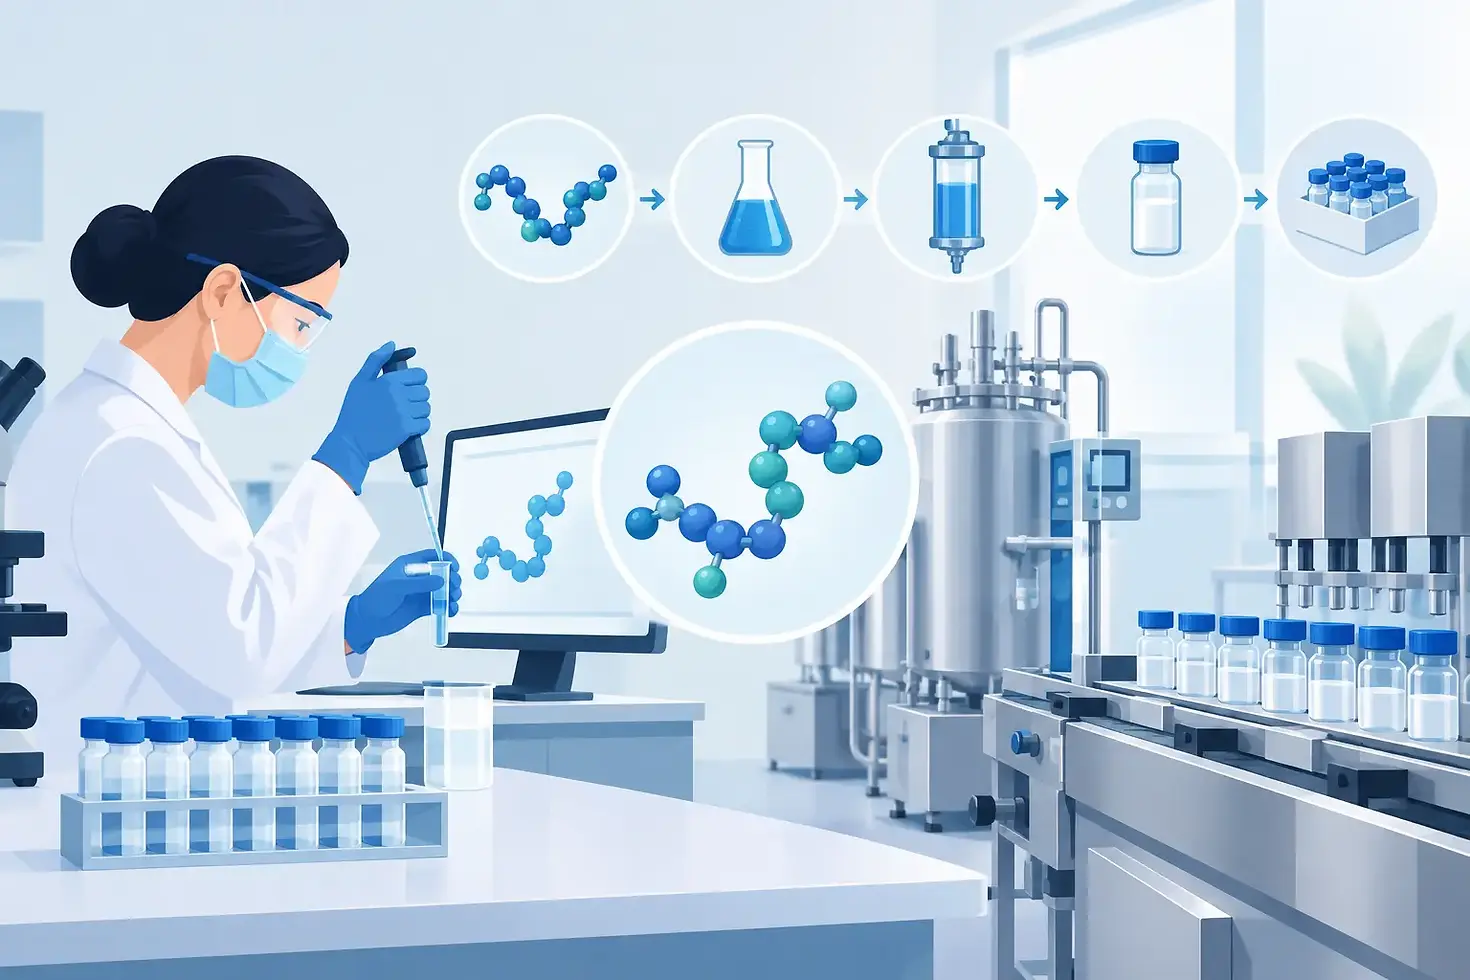
Most research peptides are made through chemical synthesis rather than isolated from biological tissue. The standard approach is solid-phase peptide synthesis, or SPPS. In this method, the growing peptide chain is anchored to an insoluble resin support while amino acids are added one at a time in the intended order.
Each amino acid arrives with temporary protecting groups. These groups prevent the wrong functional sites from reacting during assembly. After one amino acid is coupled to the chain, the temporary protection is removed, creating the next reactive site. The cycle repeats until the target sequence has been assembled.
This approach gives manufacturers control over sequence construction and is particularly useful for many short and mid-length peptides used in laboratory research. It also creates a practical challenge: every coupling and deprotection step has the potential to generate small amounts of incomplete or altered material. Process discipline matters because minor deviations can compound over a long synthesis.
Some sequences require additional planning. Amino acids with challenging side chains, hydrophobic stretches, repeated residues, disulfide bonds, terminal modifications, or unusual chemical groups can affect yield and impurity profiles. A credible manufacturing program does not treat every peptide as interchangeable. It assesses the chemistry of the individual sequence and builds controls around known risks.
Sequence Design Starts Before Synthesis
The intended peptide must be specified precisely before production begins. That includes amino acid sequence, chirality, terminal structure, salt form where applicable, expected molecular mass, and any modification such as acetylation, amidation, cyclization, lipidation, or a linker.
A single substitution can materially change a peptide's analytical profile and research behavior. The same is true for an incorrect stereochemical form of an amino acid. Documentation must therefore connect the requested structure to the manufacturing instructions, in-process records, analytical method, and final certificate for the lot.
At this stage, manufacturers also consider manufacturability. A sequence may be chemically possible to make but difficult to produce cleanly at a useful scale. The right strategy depends on peptide length, structural complexity, target quantity, and the required purity specification. Higher purity can be necessary for sensitive work, but it may reduce final yield and increase cost. There is no universal purity target that fits every research application.
Controlled Assembly and Cleavage
During solid-phase synthesis, the resin-bound chain is built through repeated cycles of amino acid addition and removal of temporary protecting groups. Materials, equipment, reaction records, and line clearance practices all influence reproducibility. Facilities operating under established quality systems use defined procedures to reduce mix-ups, cross-contamination, and avoidable process variation.
Once assembly is complete, the peptide is separated from the resin. Protective groups on reactive side chains are removed during this stage as well. The resulting crude material contains the target peptide alongside process-related impurities, including shortened sequences, deletion variants, chemically modified species, and residual reagents.
Crude material is expected at this point. The meaningful question is whether the manufacturer has a suitable purification strategy and analytical plan to separate, identify, and control what remains. A claim of high purity without a clear testing framework provides limited assurance.
Purification Separates the Target Material
Preparative chromatography is commonly used to isolate the desired peptide from crude synthesis components. The process separates compounds based on their interaction with the chromatographic system, allowing fractions containing the target material to be collected.
Purification is not merely a matter of selecting the fraction with the largest signal. The manufacturer must evaluate fraction profiles, confirm identity, and balance purity against recovery. Aggressive purification can improve a reported purity number while reducing yield. Insufficient purification may leave closely related impurities that are difficult to distinguish without appropriate analytical methods.
For more complex peptides, purification may require multiple stages or carefully optimized conditions. The goal is not cosmetic appearance. It is a defined material profile supported by data.
Analytical Testing Confirms What Was Made
Testing is where a manufacturing claim becomes evidence. The exact analytical panel should be appropriate to the peptide and intended research use, but several tools are central to quality assessment.
High-performance liquid chromatography, often HPLC or UPLC, is commonly used to assess purity and reveal related impurities. Mass spectrometry is used to confirm that the observed molecular mass aligns with the intended peptide structure. Together, these methods offer complementary information: chromatography assesses separation and profile, while mass analysis helps verify identity.
Additional testing may be appropriate based on the formulation and handling requirements. This can include peptide content, moisture, residual solvents, counterion content, microbial limits, endotoxin, appearance, reconstitution behavior, or stability-indicating assessments. Not every test applies to every lot in the same way. What matters is that specifications are justified, methods are suitable, and results are reviewed before release.
One point deserves emphasis: a purity percentage alone does not prove identity, concentration, sterility, or suitability for a particular experiment. HPLC purity is useful, but it is only one component of a complete quality picture.
Lyophilization Protects the Finished Peptide
After purification and confirmation, many peptides are converted into a dry powder through lyophilization, also called freeze-drying. The material is frozen and water is removed under controlled conditions. This format can improve handling and storage stability for many research peptides when compared with an aqueous solution.
Lyophilization is not a guarantee of indefinite stability. Storage conditions, light exposure, temperature, oxygen, moisture, peptide sequence, and salt form can all affect the finished material over time. Packaging and storage recommendations should reflect the known characteristics of the product rather than rely on a generic statement.
The dry material is then filled into appropriate containers, typically with lot traceability maintained through packaging. Controlled labeling helps prevent mix-ups and gives laboratory teams a direct connection between the vial, documentation, and test results.
Release Requires Documentation, Not Assumption
Final quality review is a separate decision point. Before release, production records, test results, deviations, and packaging information should be evaluated against established specifications. A lot should not be released simply because it looks acceptable or because a single test passes.
For buyers, the most useful documentation commonly includes the product name, lot number, reported purity, identity confirmation method, test date, and relevant handling information. A certificate of analysis should correspond to the specific lot received, not serve as a generic example from another batch.
Certified cGMP manufacturing environments and disciplined quality systems can strengthen process control, but buyers should still evaluate the evidence associated with the individual material. Facility credentials matter. Lot-specific data matters too.
What Laboratory Buyers Should Look For
A dependable supplier should be able to communicate the basics clearly: what was manufactured, how the lot was identified, which analytical methods supported release, and how the material should be handled. Vague claims, recycled documentation, or unexplained purity figures create procurement risk.
Look for consistency across product labeling, certificates, and technical descriptions. Confirm that the peptide name and stated form match the material your protocol requires. Review purity in context, especially when comparing lots or suppliers. If a study is sensitive to residual solvents, moisture, endotoxin, or a specific counterion, ask whether those attributes were evaluated rather than assuming they were included.
Domestic fulfillment can also support research continuity by reducing transit uncertainty and simplifying communication when a documentation question arises. At MARx Therapeutics, the standard is direct: research materials should be backed by disciplined manufacturing, lab testing, and clear lot accountability.
The most useful purchasing decision is rarely based on the lowest price or the highest purity number alone. Choose material whose manufacturing story can be followed from sequence to release, then document the lot in your own research records. That is how quality becomes a controlled variable instead of an unanswered question.

Comments